


Aluminum Extrusion + CNC Finishing vs. Solid Bar Stock Milling: Balancing Cost and Precision
2026-11-11
When manufacturing aluminum alloy parts, should you choose aluminum extrusion followed by CNC finishing, or mill the part directly from a solid aluminum bar? This article compares the two approaches in terms of precision, cost, deformation, production volume, and surface treatment to help procurement professionals and structural engineers make the right choice.

In custom aluminum alloy manufacturing, a common dilemma arises: should you create an extrusion die to produce a near-net-shape profile—followed by CNC finishing—or should you start with a solid aluminum bar and mill away all the excess material? At Dongguan Tengtu Aluminum Products, we offer comprehensive capabilities, including extrusion die creation, profile finishing, and five-axis milling from bar stock. In our daily operations, we frequently encounter clients who have selected an unsuitable process, leading to higher costs, part deformation, and longer lead times.
The fundamental difference between these two routes lies in the amount of material removed and the method used to form the initial blank.
Milling from solid bar stock begins with a solid workpiece, from which unwanted material is gradually removed using cutting tools. Its primary advantage is that it eliminates the need for an extrusion die; this allows for rapid prototyping and provides the flexibility to modify designs without the cost or time required to create a new die. As long as the machine’s travel range permits, parts with highly irregular cross-sections can be machined directly. This method is ideal for small-batch production, components with complex internal cavities or intricate structures, parts with cross-sections unsuitable for extrusion, and R&D prototyping.
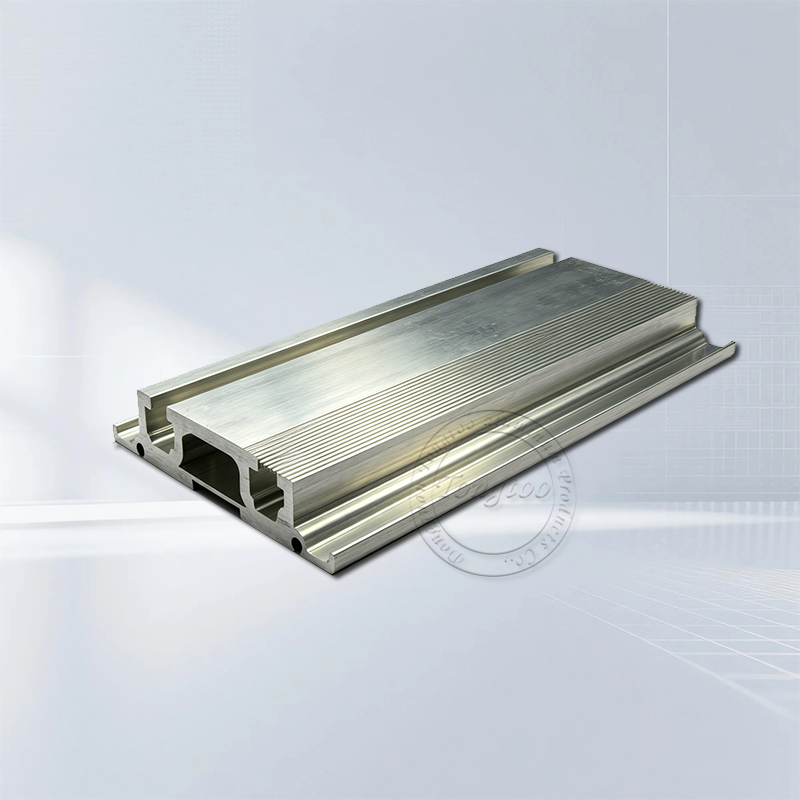
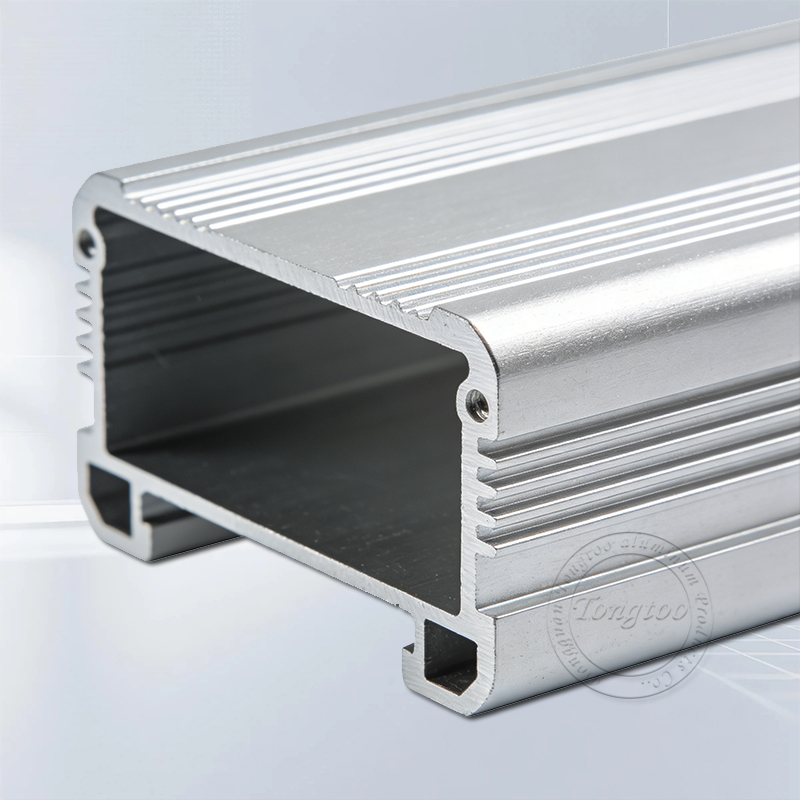
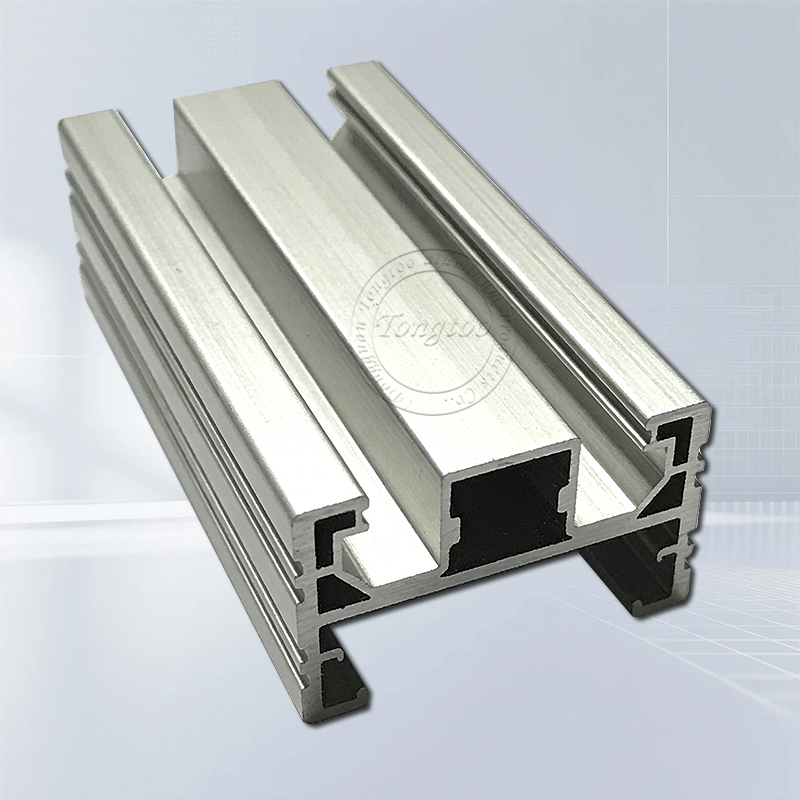
However, the drawbacks are equally significant. Milling from bar stock results in substantial material waste—essentially, every bit of aluminum swarf represents a direct cost. The high volume of material removal also leads to longer machining times, which naturally drives up the price. Furthermore, solid bar stock often contains high levels of internal residual stress; when a large amount of material is removed, this stress can be released, causing the part to warp or deform—a risk that is particularly pronounced in thin-walled components. Even if stress-relief processes are incorporated, they add extra steps and extend the production cycle. Additionally, if a part is very long, sourcing the appropriate bar stock and securing it for machining can present further challenges. Aluminum extrusion combined with CNC finishing begins with an extrusion die, which produces a profile closely approximating the final part's contour. The cross-section is already largely consistent with the finished component, leaving only a small margin for subsequent machining. Extrusion easily creates features such as cooling fins, elongated cavities, hollow structures, and multi-ribbed cross-sections—geometries that would be time-consuming, or even impossible, to produce by milling from solid bar stock.
In terms of cost, the extrusion process features a critical threshold: while initial investment—specifically for the extrusion die—is high, the per-unit cost drops rapidly as production volume increases. Material utilization is significantly higher, with minimal machining allowance, reduced CNC processing time, and less waste in the form of aluminum chips. Furthermore, because extruded profiles undergo in-line quenching with well-controlled internal stress, they offer superior stability for long, thin-walled components compared to parts milled from solid stock. This makes the process ideal for products such as lighting housings, heat sinks, long guide rails, and elongated bases for automation equipment. Common aluminum alloys used for extrusion include the 6063 and 6061 series.
However, extrusion has its limitations. It imposes strict constraints on cross-sectional geometry; features like undercuts, enclosed narrow cavities, or abrupt transitions between extremely thick and thin sections are difficult or impossible to extrude. Once the cross-section is finalized, any subsequent design changes usually require modifying or replacing the die—a costly process that makes extrusion unsuitable for the R&D phase, where designs may frequently evolve. Additionally, extrusion processes are subject to technical constraints, such as minimum wall thickness and specific width-to-height ratio limits, meaning not every cross-sectional design can be successfully extruded.
Comparison of Precision
Many engineers mistakenly assume that milling from solid bar stock inherently yields higher precision, but this is not necessarily the case.
Milling from solid bar stock: While theoretically capable of achieving very tight geometric tolerances, the process carries risks related to internal stress. If a large volume of material is removed without proper stress-relief measures, the part may gradually deform over time, leading to dimensional drift—making it difficult to maintain consistent tolerances. This method is best suited for components requiring high-precision localized features, such as specific holes, inclined surfaces, or complex internal cavities, where precision is managed through specialized tooling and carefully planned toolpaths. Extrusion + CNC: Extrusion alone can only define the general profile of a part, with relatively loose tolerances for the raw extruded blank. The final precision is achieved entirely through subsequent CNC finishing. As long as the machining allowance is uniform and the fixturing is stable, critical dimensions, hole positions, and mating surfaces can all be manufactured to high-precision standards. This approach is particularly advantageous for long, linear components, offering superior overall rigidity and a lower risk of chatter marks (vibration patterns) often associated with milling.
Surface Treatment Compatibility
Both methods support sandblasting, brushing, anodizing, and Alodine (chemical conversion coating).
Extruded profiles: 6063 alloy extrusions offer a refined, lustrous finish when anodized, making them the preferred choice for decorative exterior components.
Solid bar stock: Typically 6061 or 7075 alloys; these are well-suited for hard-coat anodizing and are more commonly used for structural, load-bearing components.
Selection Criteria: A Quick Guide
Choose Extrusion + CNC Finishing when:
Production volume is high, the cross-section is fixed, and long-term production is planned.
The part is long, acts as a heat sink, features hollow sections, or incorporates complex finned cooling structures.
High aesthetic standards are required, necessitating a high-quality anodized finish.
The goal is to minimize per-unit costs and reduce material waste.
Choose Milling from Solid Bar Stock when:
You are in the prototyping or small-batch production phase, or the design is still evolving with frequent shape changes.
The cross-section is complex or includes undercuts that cannot be formed via extrusion.
The parts are small and the quantity is low, making the investment in an extrusion die uneconomical.
High-strength aerospace-grade alloys (such as 7075) are required—materials that are difficult or costly to extrude.
Practical Advice: Avoiding Common Pitfalls
Clients often fall into one of two extremes: insisting on milling from solid bar stock for high-volume production (leading to unnecessary budget waste), or paying for expensive extrusion dies before the design is finalized (resulting in high costs if the design—and thus the die—needs to be modified later). At Tengtu Aluminum Products, upon receiving your drawings, we first evaluate the production volume, cross-sectional profile, and tolerance requirements. If the part is suitable for extrusion, we provide two distinct options, detailing the respective costs for tooling and per-unit processing. For R&D prototyping, we recommend CNC milling from solid bar stock to ensure a quick turnaround; once the design is finalized, we can transition to extrusion for mass production—balancing R&D efficiency with cost-effective, large-scale manufacturing.
FAQ
For a run of only a few dozen pieces, should I choose extrusion or bar stock milling?
If the cross-section is simple and the tooling cost is low, extrusion may be an option. In most cases, however, small-batch production is better handled via CNC milling from bar stock, as this avoids the expense of creating a custom extrusion die.
What level of tolerance can be achieved after precision machining an extruded profile?
Critical mating dimensions are controlled via CNC machining, allowing for standard precision-machined tolerances—comparable to those achieved when machining from solid bar stock. The raw extruded profile itself is not intended to provide high-precision dimensions.
Are extruded parts more prone to deformation?
If the extrusion process is stable and the machining allowance is uniform, extruded profiles can actually be more dimensionally stable than parts machined from solid stock (which often require significant material removal). However, if the cross-sectional design is poorly conceived, the extrusion process itself can lead to warping or twisting.
Can I use bar stock to prototype and validate the design before investing in an extrusion die?
This is the most reliable approach in the industry, and it is the strategy we frequently recommend to our international clients.
RELATED NEWS
-
Does Extruded Aluminum Rust?
If you’re sourcing metal profiles for your next project, one question always comes up: does extruded aluminum rust?
-
What Is a 5-Axis CNC Machine? When Should You Use 5-Axis Machining?
Clients new to precision machining often ask: "What is a 5-axis CNC machine, and do my parts actually require 5-axis processing?" Simply put, while a 3-axis machine can only move its cutting tool along the X, Y, and Z axes, a 5-axis machine adds two rotational axes—either via the worktable or the spindle.
-
How to Select Aluminum Extruded Profiles: Key Points Often Overlooked
Procurement professionals frequently reach out with drawings to inquire about aluminum profiles. Many focus solely on price, overlooking critical factors like alloy grade, cross-sectional tolerances, and surface treatment—only to discover upon delivery that the profiles fail to meet assembly or functional requirements.
-
Rising Demand for Industrial Aluminum Profiles: T-Slot and 4040 Series for Automation Frameworks
In the realm of industrial aluminum profiles, T-slot extrusions—particularly the 4040 specification—are the most frequently used components in factory automation projects.
-
What is the next growth point for aluminum alloy precision machining driven by new energy and intelligent hardware dual wheel drive?
The opportunities for precision machining no longer only come from products with large quantities, but also from orders with complex structures, high requirements, and a greater emphasis on collaboration. This means that suppliers need to transform from "processing plants" to "process solution providers", reflecting their value in drawing evaluation, sampling, and DFM processes.
-
CNC machining of automotive parts - precision, material and batch quality control
The requirements for processing automotive parts can be summarized as "both precision and consistency". Whether it is brackets, shells, or irregular structural components, the quality of batch delivery is stable, which tests suppliers better than doing a single piece well.
-
Precision CNC Machining and Aluminum Profile Mold Making: Tengtu Aluminum Products Offers Custom Solutions Across Multiple Industries
As a lightweight engineering material, aluminum alloy is seeing growing application in sectors such as home appliances and 3C electronics.
-
CNC Machining for 3C Electronics: Aluminum Alloy Housings & Thermal Modules; Custom Aluminum Profile Mold Services
The consumer electronics industry demands high precision, superior thermal performance, and premium aesthetic quality for aluminum alloy components.
-
Custom CNC Machining of Aluminum Alloy Home Appliance Parts & One-Stop Aluminum Profile Mold Solutions
Dongguan Tongtoo Aluminum Products Co., Ltd. specializes in precision aluminum alloy machining.
-
Why 6061-T6 aluminum alloy is the Benchmark Material for CNC Machining
In the field of CNC machining, material selection directly impacts precision, efficiency, and cost. Among hundreds of aluminum alloys, 6061-T6 holds a unique position—often hailed as the "King of CNC Machining" and the "Universal Industrial Alloy."
-
What are the differences between 3-axis, 4-axis, and 5-axis CNC milling?
In precision manufacturing, the choice between 3-axis, 4-axis, and 5-axis CNC milling directly impacts a part's manufacturability, precision, and cost. The core differences lie in the number of motion axes and degrees of freedom, which determine the types of geometric features that can be machined.
-
Large-Scale Order of Custom Extruded Aluminum Profiles Enters Full Inspection Phase:A Comprehensive Record of the Precision Manufacturing Process—From Extrusion to Black Anodized Finished Product
In August 2026, as the final batch of products completed the black anodizing process and moved to the full inspection workshop, a large-scale order for custom (non-standard) extruded aluminum profiles—undertaken by our company—officially entered the final pre-shipment quality verification stage.
-
Dongguan Tongtoo Aluminum Products Co., Ltd. Acquires Two Brother U500XD2-5AX 5-Axis CNC Machining Centers, Elevating Precision Manufacturing Capabilities
August 11, 2026 — To further enhance its precision aluminum alloy machining capabilities and accelerate its transformation toward intelligent manufacturing, Dongguan Tongtoo Aluminum Products Co., Ltd.
-
Fully In-House Capabilities Across The Entire Value Chain—From Mold Making And Extrusion To Precision Machining—Custom Aluminum Profiles Have Arrived.
It’s a busy scene at our workshop entrance today; a shipment of raw aluminum profiles—custom-made for clients—has just arrived, and the team is hard at work unloading.
-
Why are grinding, polishing, and brushing performed after CNC machining aluminum alloys? A comprehensive analysis of these three key surface preparation processes.
Aluminum alloys are easy to machine and offer a wide range of surface treatment options, making them widely used in sectors such as consumer electronics and automotive manufacturing.
-
CNC Machining vs. Injection Molding: How to Choose the Right Manufacturing Process for Your Aluminum Alloy Parts?
During product development, engineers and procurement professionals often face a critical decision: Should I choose CNC machining or injection molding? These are two of the most widely used production processes in modern manufacturing.
-
Delivering an Order of 5,000 Units 15 Days Early: Real-World Application of a 4-Axis CNC Machining Center and Custom Fixture
A detailed look at a high-efficiency batch processing solution: completing drilling and end-face milling in a single setup.
-
Common Issues in Aluminum Profile CNC Machining: Drill Runout, Stripped Threads, and Uneven Chamfers—How to Solve Them?
When performing CNC machining on aluminum profiles, one inevitably encounters recurring issues on a daily basis. No matter how flawless the technical drawings may appear, problems often surface the moment the workpiece hits the machine tool.
-
Breaking Through Process Bottlenecks: An Innovative Solution for Stamping and Anodizing Small Aluminum Alloy Discs with CD Patterns
In the field of precision machining for aluminum alloys, the integration of anodizing and CD pattern (concentric circle) processes has long presented a significant challenge in the production of cosmetic components.
-
Cost Reduction and Efficiency Gains at the Source: 10 Golden Rules for DFM Optimization of Aluminum Parts for CNC Machining
Understanding the physical limits of CNC machining is the first step for engineers and procurement specialists looking to reduce costs. DFM—Design for Manufacturability—addresses precisely this issue: integrating machining feasibility into the design phase rather than waiting until the blueprints reach the factory to discover problems.
-
From Aluminum Profile Die Opening to Extrusion: How Die Design Determines Profile Precision
In the process of customizing aluminum profiles, clients are typically most concerned with three key questions: Is the dimensional accuracy precise? Is the straightness satisfactory?
-
Explains the Advantages of 5-Axis CNC Parts Machining
This advanced machining technology allows companies to produce highly complex, accurate, and durable components across industries such as aerospace, automotive, electronics, and medical devices.
-
DongGuan TongToo Aluminum Products Co., Ltd. Explains the Benefits of Custom CNC-Machined Aluminum Alloy Parts
DongGuan TongToo Aluminum Products Co., Ltd., a leading manufacturer of precision aluminum components, is highlighting the growing importance of Custom CNC-Machined Aluminum Alloy Parts in modern manufacturing.
-
From aluminum bars to finished products: We provide one-stop aluminum alloy component solutions including extrusion, CNC machining, and anodizing
Our company integrates three core processes: aluminum alloy extrusion, CNC precision machining, and anodizing surface treatment, providing customers with a truly one-stop service from aluminum bars to finished products.
-
How can aluminum profile CNC deep processing factories achieve efficient delivery of small batches and multiple varieties?
When a factory truly integrates "fast response, stable quality, and controllable cost", it can take the lead in the wave of personalized customization - even a 20 piece aluminum profile frame order can be delivered to customers on time with batch cost and standardized cycle. This is the ultimate competitiveness in the field of precision machining of aluminum alloys in the future.
-
How Brother CNC Enhances Our Competitiveness in Aluminum Alloy Machining
In the realm of precision manufacturing, the choice of equipment directly determines the ultimate potential of a product. Recently, our company officially commissioned two newly acquired Brother high-speed machining centers.
-
Happy Start to Work!
Dongguan Tongtoo Aluminum Products Co., Ltd. Embarks on a New Journey in 2026.
-
Is Anodized Aluminum Conductive? Unveiling the Impact of Surface Treatment on Conductivity
A common question is: Is anodized aluminum still conductive? This article will delve into the conductive properties of aluminum before and after oxidation treatment and analyze relevant industry technologies.
-

What Are The Differences Between CNC Machining And 3D Printing?
In modern manufacturing, CNC machining and 3D printing are two core digital manufacturing technologies, both capable of transforming design models into physical parts through computer programs.
-
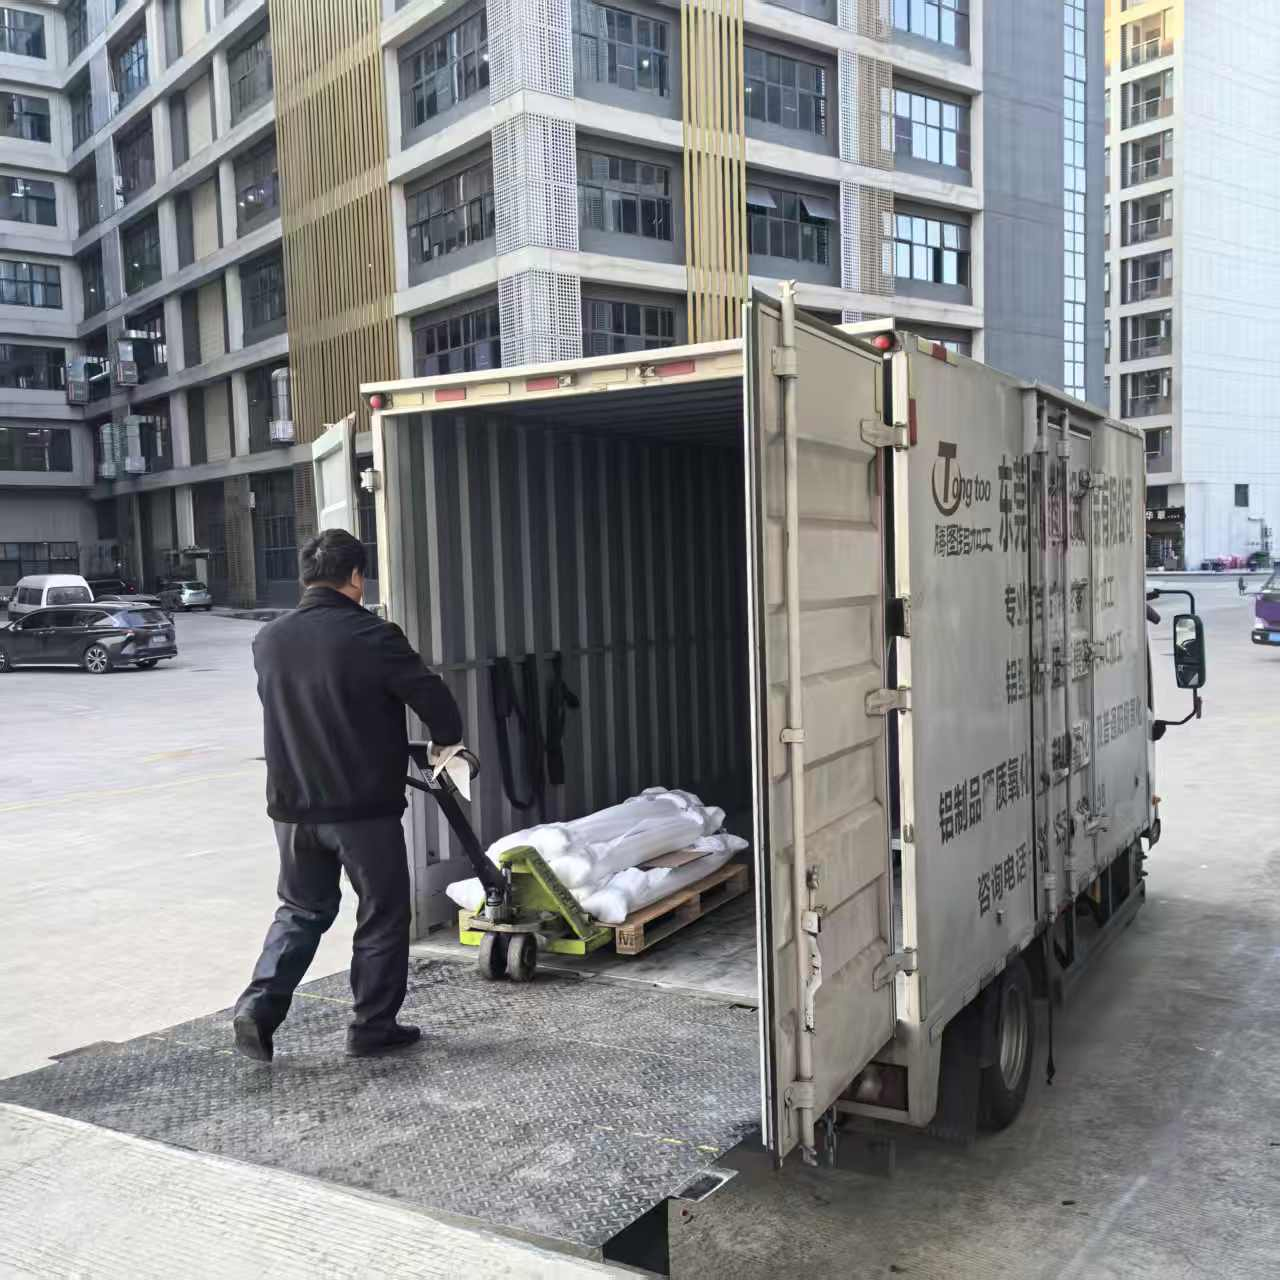
Dongguan Tongtoo Aluminum Products Co., Ltd. Successfully Delivers First Batch of Precision Aluminum Profile Samples for a Large-Volume Order: A Milestone from Collaborative Development to Mass Production Launch
Recently, our company's major cooperation project with an international client has reached a critical milestone – the first batch of engineering samples for a large-volume order of custom aluminum profiles has been successfully produced, inspected, and delivered.
-
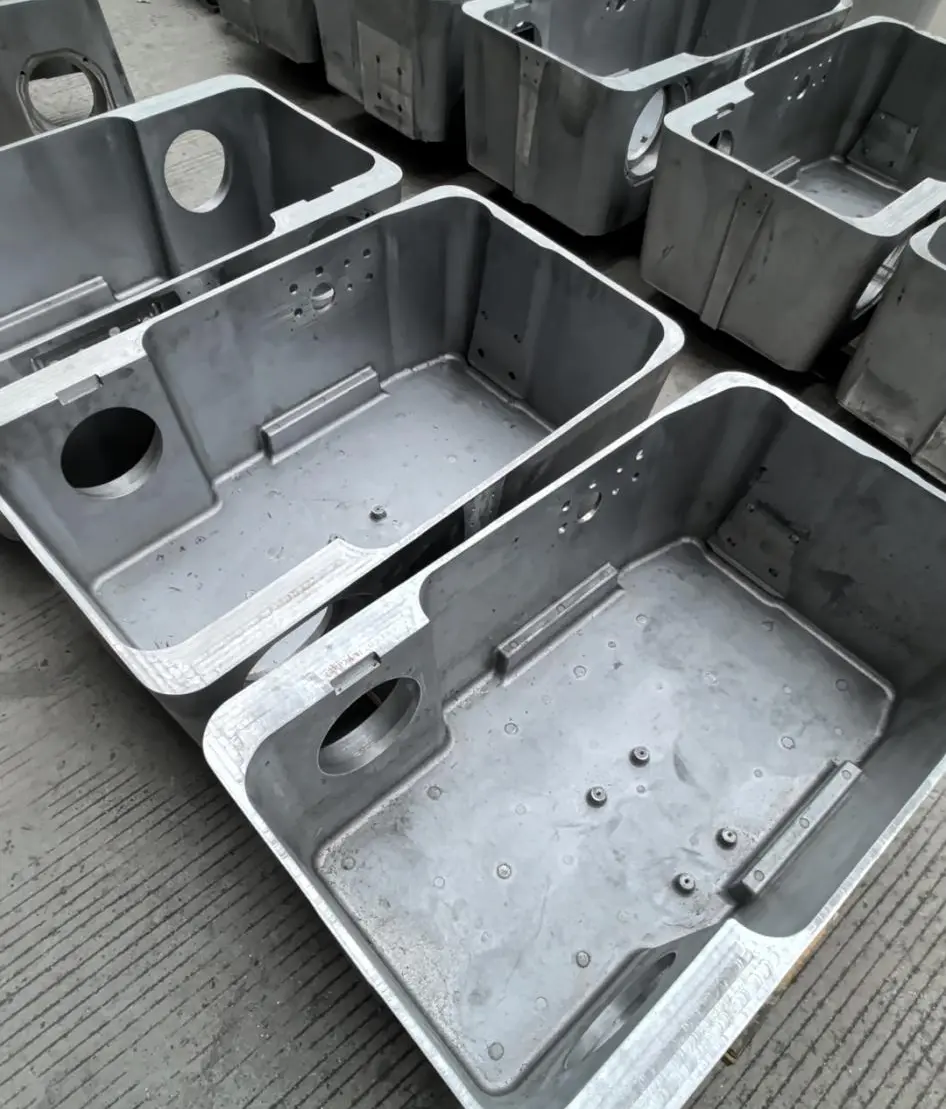
Large Cavity Machining Order Completed and Shipped on Time
A batch of large cavity machining parts we undertook has been fully machined, passed quality inspection, and shipped to the customer on time recently.
-
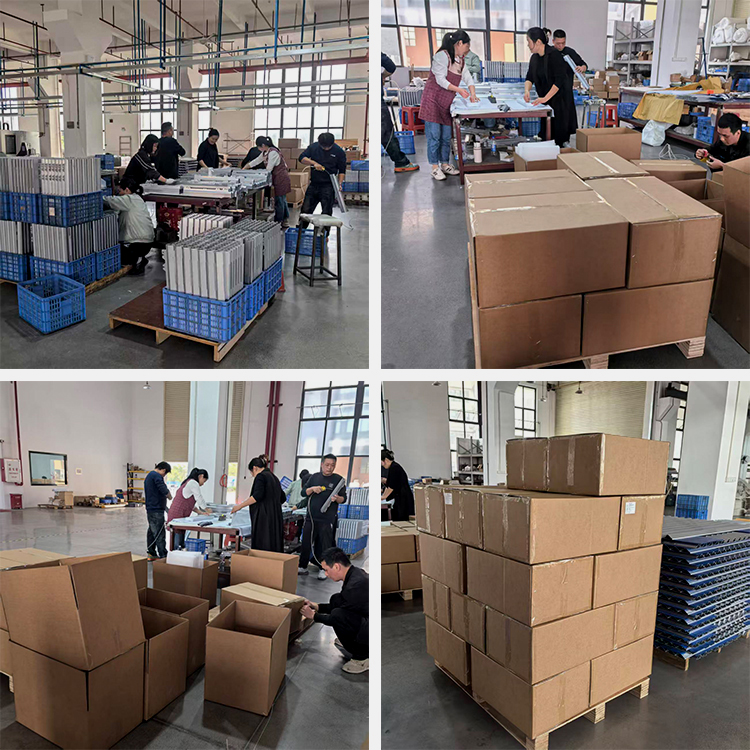
The CNC Machining Order For Automotive Parts Has Been Successfully Completed And Delivered On Schedule
The company has recently completed the production of a batch of high-precision CNC machined parts, all of which have passed inspection and have been delivered to customers on schedule. This batch of parts is applied in the automotive industry and has clear requirements for machining accuracy and delivery time.
-
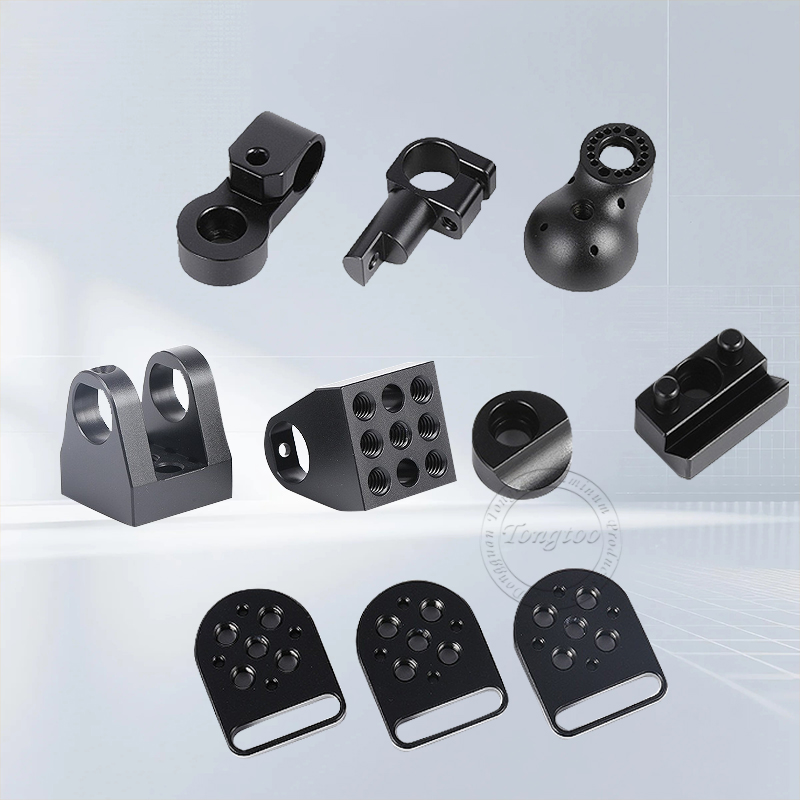
Large-Scale CNC Machining Gains Global Momentum as Demand for Precision Industrial Components Grows
As global industries move toward higher efficiency and advanced automation, Large-Scale CNC Machining is becoming increasingly crucial for the production of oversized components used in heavy equipment, energy systems, transportation, and industrial infrastructure. With manufacturers prioritizing durability, accuracy, and operational reliability, large-format machining capabilities—especially in producing high-quality CNC Milling Parts—are now at the center of modern industrial development.
-
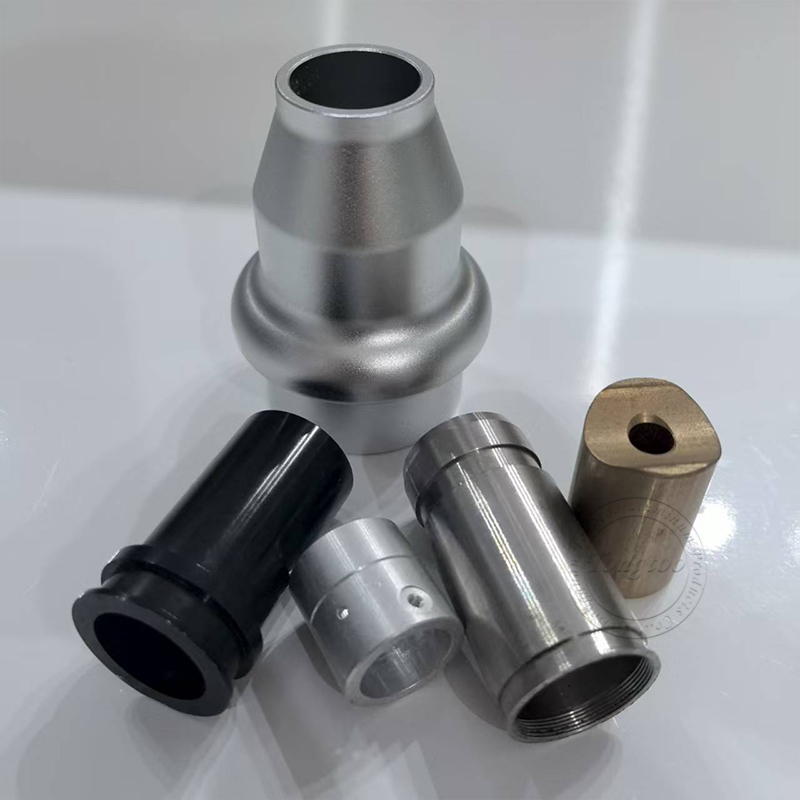
Growing Demand for CNC Turned Shaft Components Drives Innovation in Precision Manufacturing
As industries worldwide push for higher accuracy, durability, and efficiency in mechanical systems, CNC turned shaft components are becoming increasingly essential across sectors such as automotive, industrial machinery, robotics, and home appliances. These components, manufactured through advanced machining technologies, play a critical role in transmitting motion, supporting rotational movement, and ensuring stable mechanical performance. With this rising demand, the market for high-quality CNC Turning Parts is experiencing significant growth and rapid technological advancement.
-
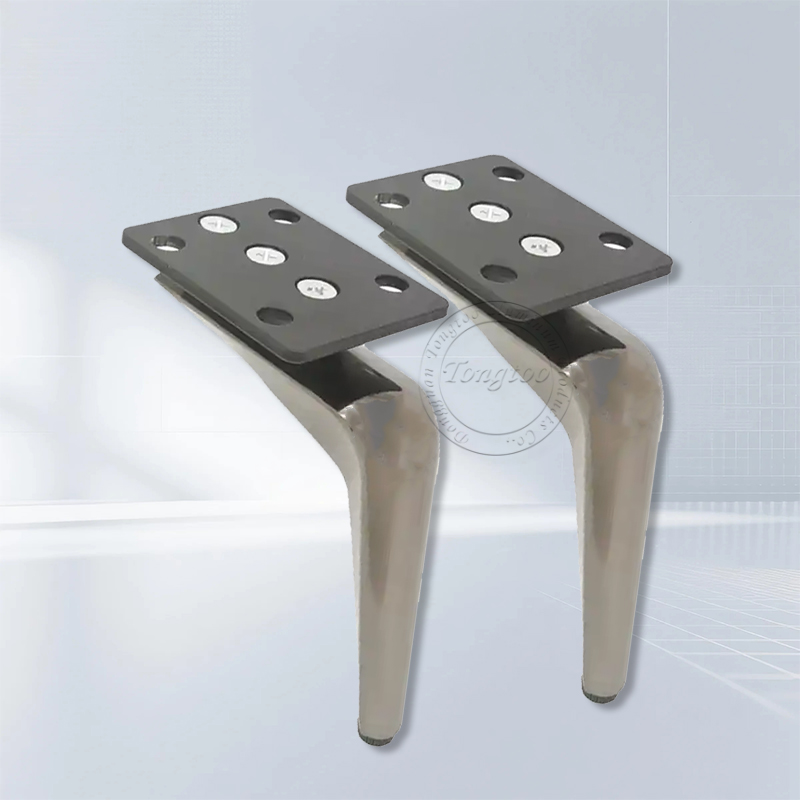
OEM CNC Machining Parts for Furniture Hardware Gain Momentum as TongToo Aluminum Products Expands Global Reach
The global furniture industry is undergoing a significant shift toward higher-quality, more durable, and customizable components, driving increased demand for OEM CNC machining parts for furniture hardware. Among the manufacturers leading this trend is TongToo Aluminum Products, a brand that has built a strong reputation for delivering precision-engineered parts designed to enhance both the functionality and aesthetics of modern furniture.
-
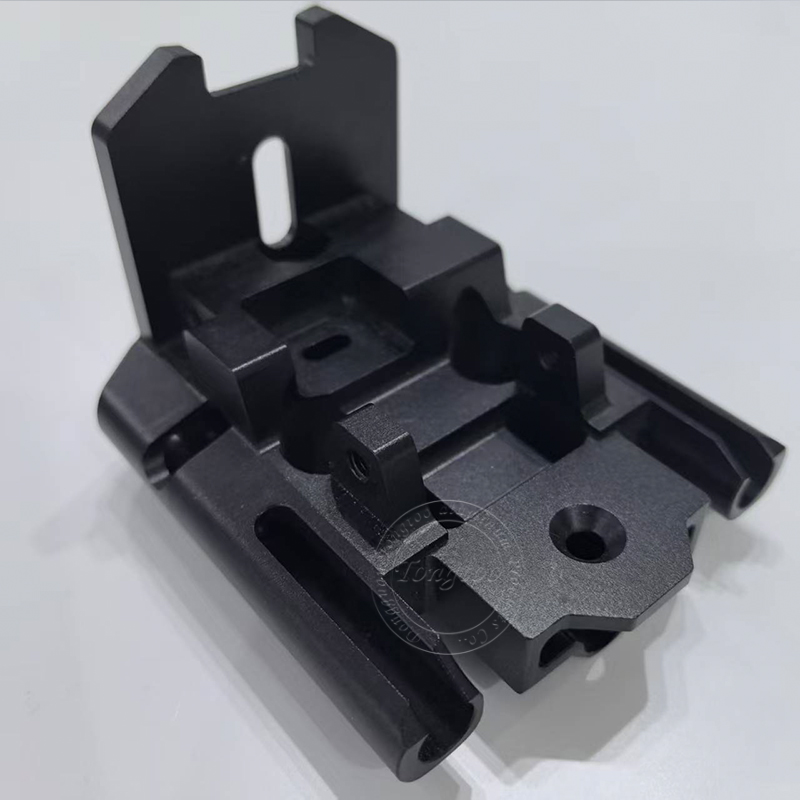
High-Precision Aluminum Alloy CNC Milling Services Gain Industry Attention as Demand for Lightweight Components Rises
As global manufacturing continues to shift toward lightweight, high-strength materials, High-Precision Aluminum Alloy CNC Milling Services are emerging as a key driver of innovation across multiple industries. From consumer electronics and automotive engineering to medical devices, manufacturers are increasingly relying on advanced machining technologies to produce durable, cost-effective CNC Milling Parts made from premium aluminum alloys.
-
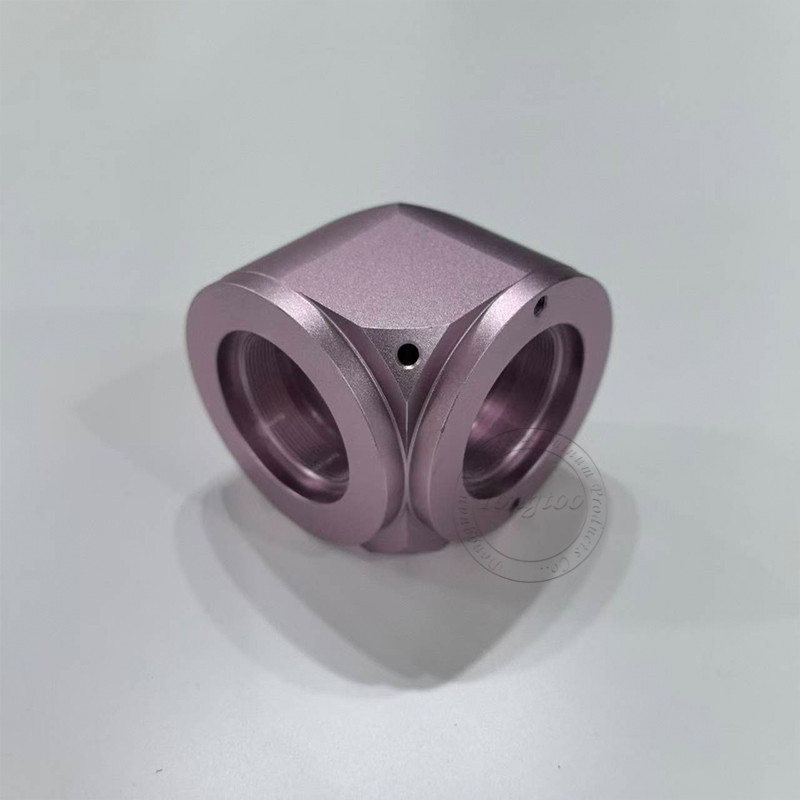
High-Precision CNC Milling Service Gains Momentum as Industries Push for Greater Accuracy
As global manufacturing continues its shift toward higher efficiency and tighter tolerances, High-Precision CNC Milling Services are experiencing a significant surge in demand. From automotive to consumer electronics and medical equipment, more industries are turning to advanced machining capabilities to produce reliable, complex, and high-performance components. At the center of this trend is the growing need for CNC Milling Parts that deliver exceptional accuracy, consistency, and durability.
-
Rising Demand for Small and Medium Batch Parts Machining as Industries Push for Flexibility and Precision
As global manufacturing shifts toward customization, rapid prototyping, and short production cycles, the need for small and medium batch parts machining is rapidly increasing across multiple sectors. From electronics and automotive to medical devices and industrial equipment, companies are prioritizing production models that deliver faster turnaround, tighter tolerances, and greater cost efficiency. This trend is driving renewed attention to advanced machining technologies, especially in the field of CNC Milling Parts.
-

How to Significantly Reduce CNC Machining Costs?
In a highly competitive manufacturing environment, the ability to control costs in precision parts machining directly determines a company's core competitiveness. As a core piece of equipment in modern manufacturing, the operating costs of CNC machining centers directly impact product profit margins.
-
Aluminum Alloy Components Elevate the Quality and Design of Modern Home Appliances
As the home appliance industry advances toward smarter, more durable, and aesthetically refined products, aluminum alloy has become the material of choice for leading manufacturers. From kitchen essentials to personal care devices, aluminum alloy components offer unmatched strength, thermal conductivity, and design flexibility, giving home appliances a new standard of quality and longevity.
-
TongToo Aluminum Products Leads the Industry in CNC Aluminum Product ODM Solutions
In the era of smart manufacturing and global customization, TongToo Aluminum Products has become a leading name in CNC Aluminum Product ODM services. With years of experience in precision machining and product development, the company provides comprehensive one-stop solutions—from design and prototyping to full-scale production—meeting the diverse needs of international clients in electronics, automotive, aerospace, and consumer product industries.
-
TongToo Aluminum Products: A Trusted CNC Turning Machining Parts Factory Delivering Precision and Quality
As global industries continue to demand higher standards of precision and efficiency, TongToo Aluminum Products has established itself as a leading CNC Turning Machining Parts factory dedicated to excellence in modern manufacturing. With advanced equipment, skilled engineers, and a commitment to innovation, TongToo delivers superior machining solutions for industries such as electronics, automotive, and communications.
-
TongToo Aluminum Products - A Leading CNC Turning Parts Factory Driving Precision Manufacturing Forward
In the era of intelligent manufacturing, TongToo Aluminum Products has emerged as a trusted name in the precision machining industry. As a professional CNC Turning Parts factory, the company is dedicated to producing high-quality, high-precision metal components that meet the growing demands of global industries such as electronics, automotive, and optics.
-
Precision and Performance: The Expanding Role of CNC Turning Parts in Modern Manufacturing
In today’s high-precision manufacturing industry, CNC Turning Parts have become indispensable components across various sectors, from automotive to optics and electronics. With the rapid development of digital manufacturing and automation, CNC turning technology continues to evolve, offering exceptional accuracy, consistency, and productivity for complex part production.
-
The Growing Role of Aluminum Alloy in 3C Electronics Manufacturing
In today’s rapidly evolving 3C electronics industry—covering computers, communications, and consumer electronics—manufacturers are increasingly turning to aluminum alloy materials for their superior performance and design flexibility. From laptops to mobile devices and smart audio systems, aluminum alloys are setting new standards for durability, aesthetics, and heat dissipation.
-
The Expanding Applications of Aluminum CNC Machining in Modern Industry
In today’s rapidly advancing manufacturing world, Aluminum CNC Machining has become an essential process driving precision, efficiency, and innovation across multiple industries. Combining the strength and versatility of aluminum with the accuracy of CNC (Computer Numerical Control) technology, this process enables manufacturers to produce high-quality components for a wide range of applications—from automotive to electronics and medical devices.
-
Aluminum CNC Machining: Redefining Precision and Efficiency in Modern Manufacturing
In the age of advanced manufacturing, Aluminum CNC Machining has become a cornerstone technology that drives innovation, precision, and efficiency across multiple industries. From automotive to electronics and medical equipment, this machining process enables the creation of complex, high-performance components that meet the exacting standards of modern engineering.
-
TongToo Aluminum Products Leads Innovation in Custom CNC Milling Parts Manufacturing
In today’s precision-driven manufacturing world, TongToo Aluminum Products is setting new standards in the production of custom CNC milling parts. With cutting-edge technology, expert craftsmanship, and a commitment to excellence, the company provides high-quality, tailor-made milling components that meet the complex needs of modern industries.
-
TongToo Aluminum Products Expands Precision Manufacturing with Custom CNC Turning Parts
In the fast-evolving world of precision engineering, TongToo Aluminum Products continues to stand out as a trusted manufacturer of custom CNC turning parts. With a strong focus on innovation, quality, and customer satisfaction, the company is providing high-precision components that meet the growing demands of industries such as automotive,medical equipment, and electronics.
-
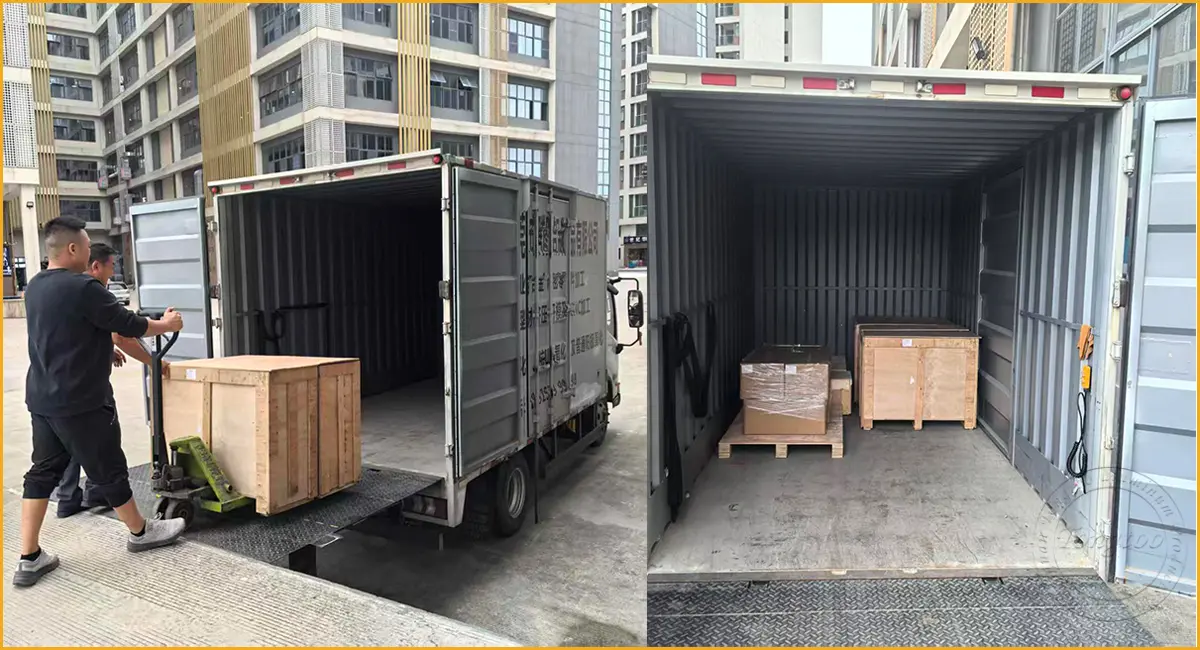
A Batch of Precision Aluminum Alloy Parts Has Been Successfully Shipped to a US Customer.
This afternoon, a batch of customized aluminum alloy parts for a US customer completed all subsequent processing steps, was successfully packaged, and handed over to a logistics company for immediate shipment to the US.
-
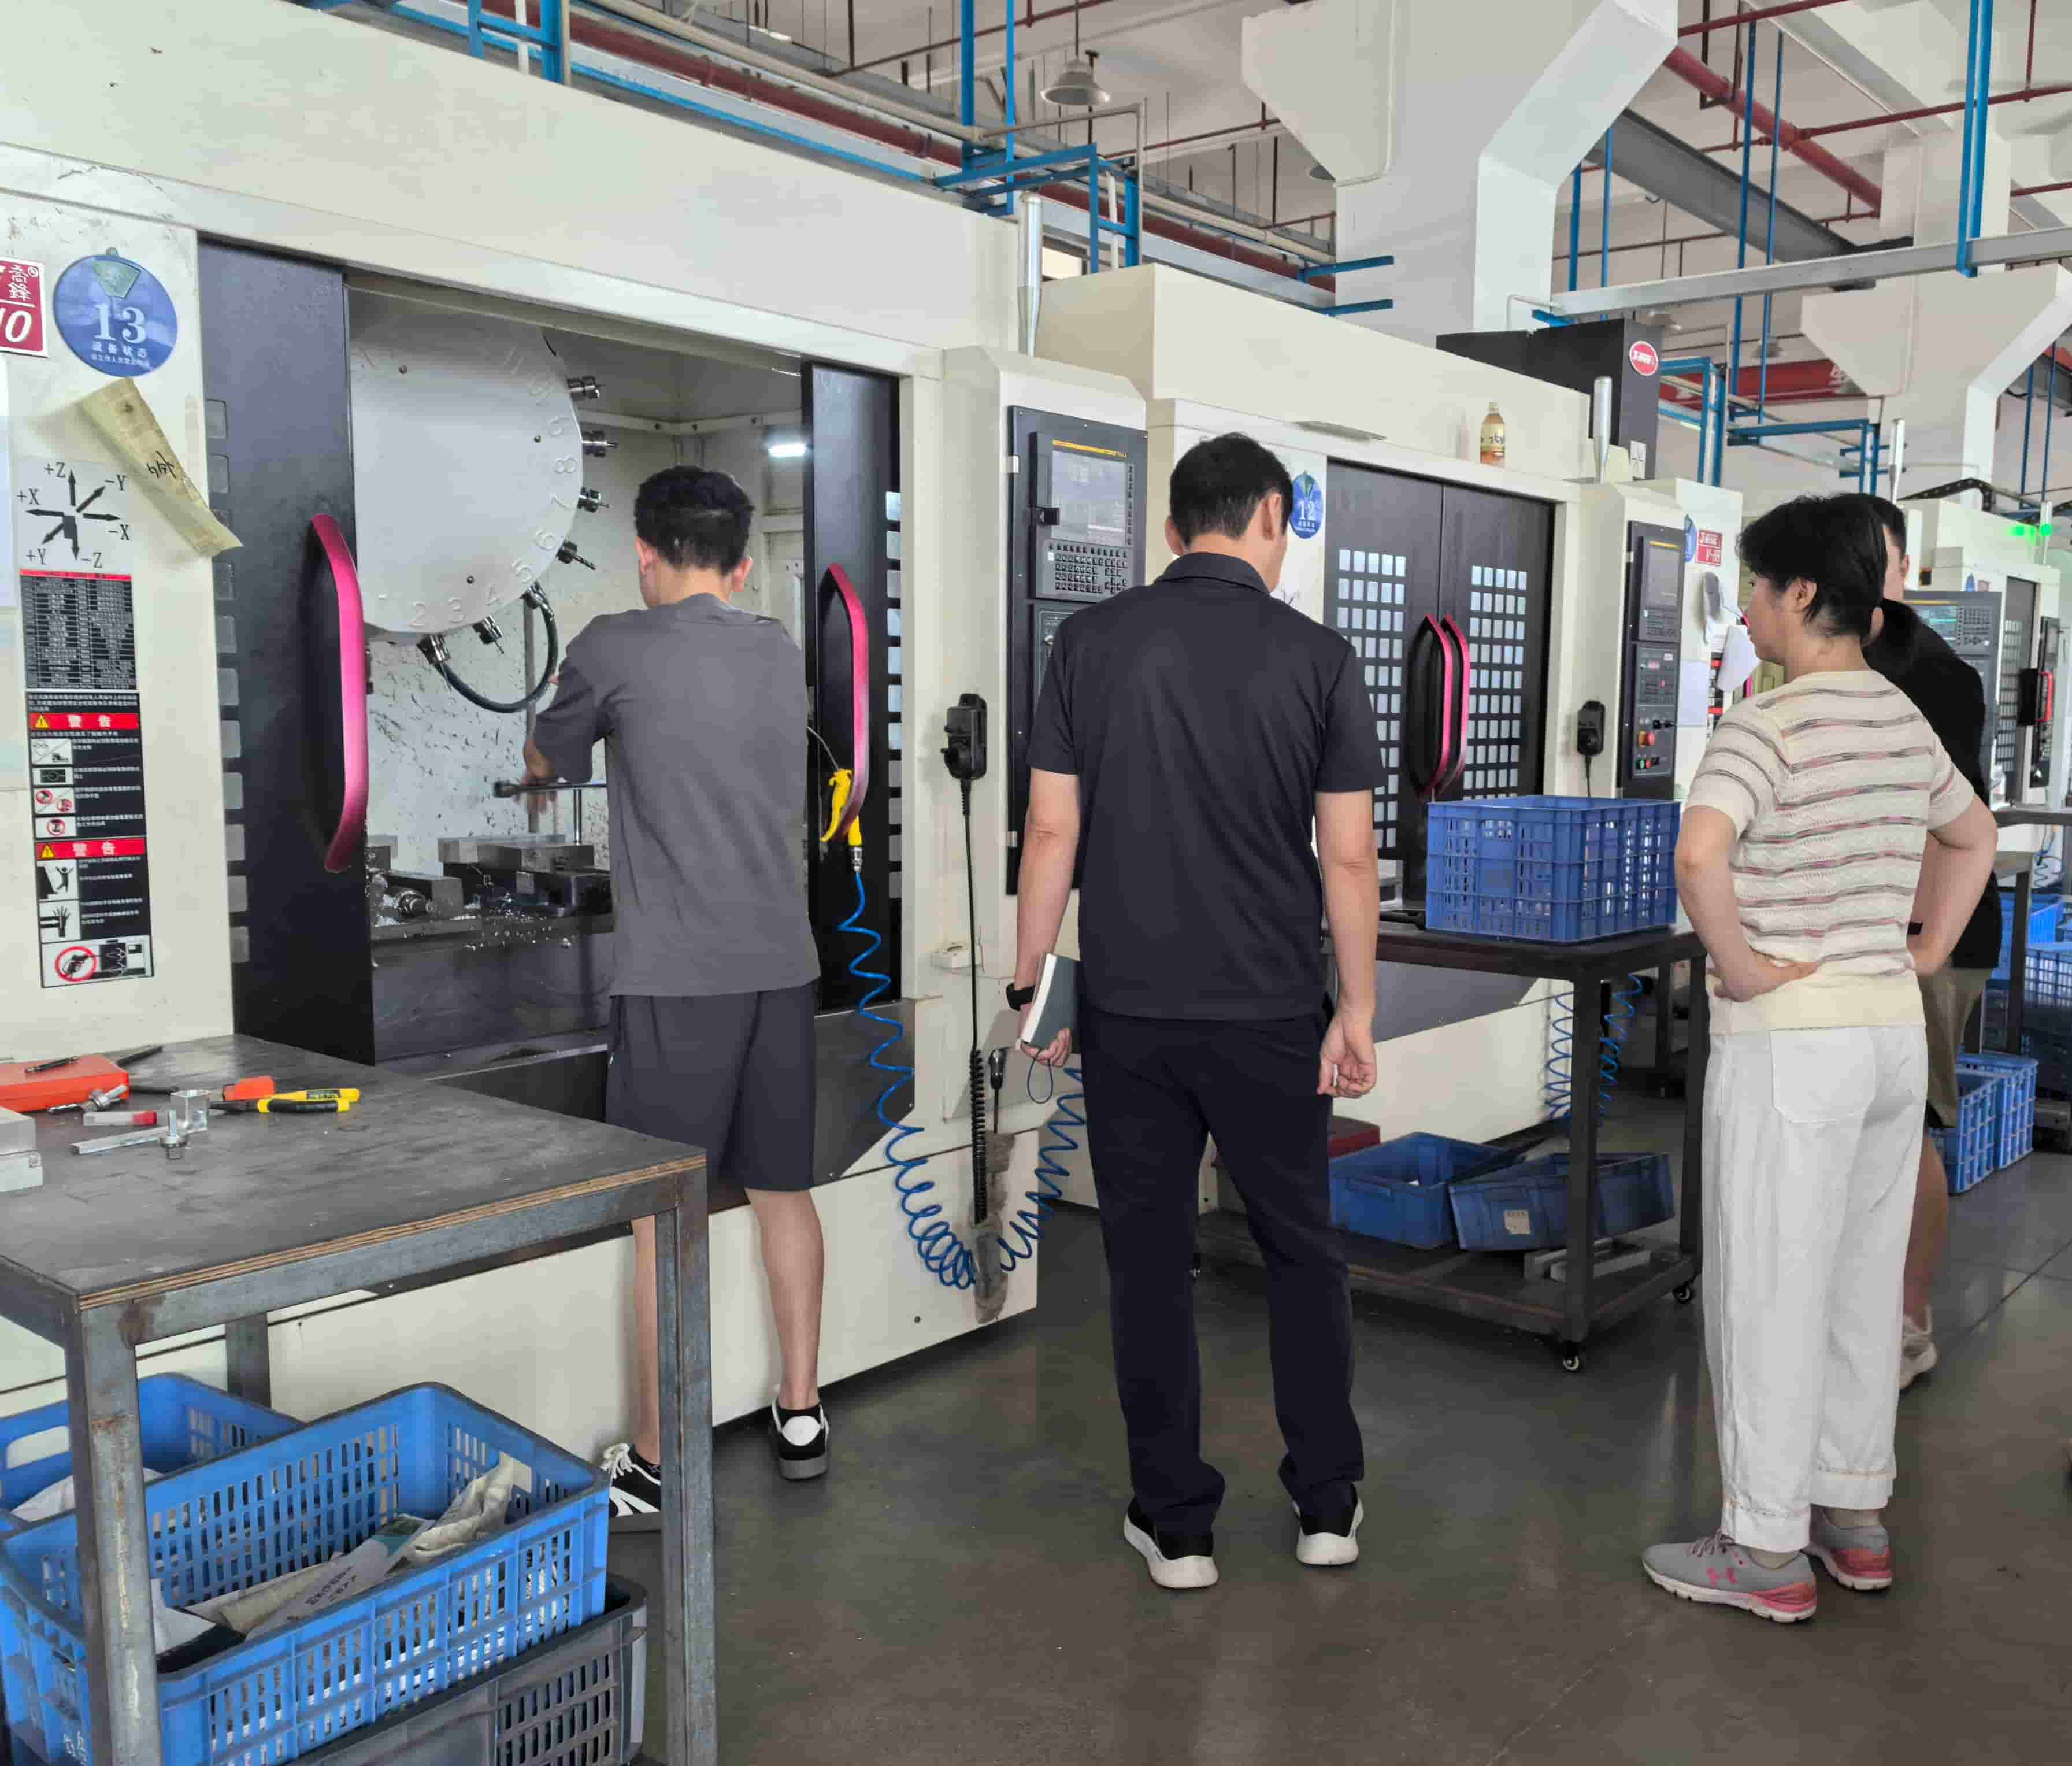
Representatives From A Renowned Korean Company Visited Our Factory
Recently, representatives from a renowned Korean electronics company visited our company to gain a first-hand understanding of our production capabilities, process flow, and quality management system. Accompanied by our Sales Director Xie Li and General Manager Wang Zongchao, the Korean customers enjoyed an in-depth tour of our modern production facility.
-
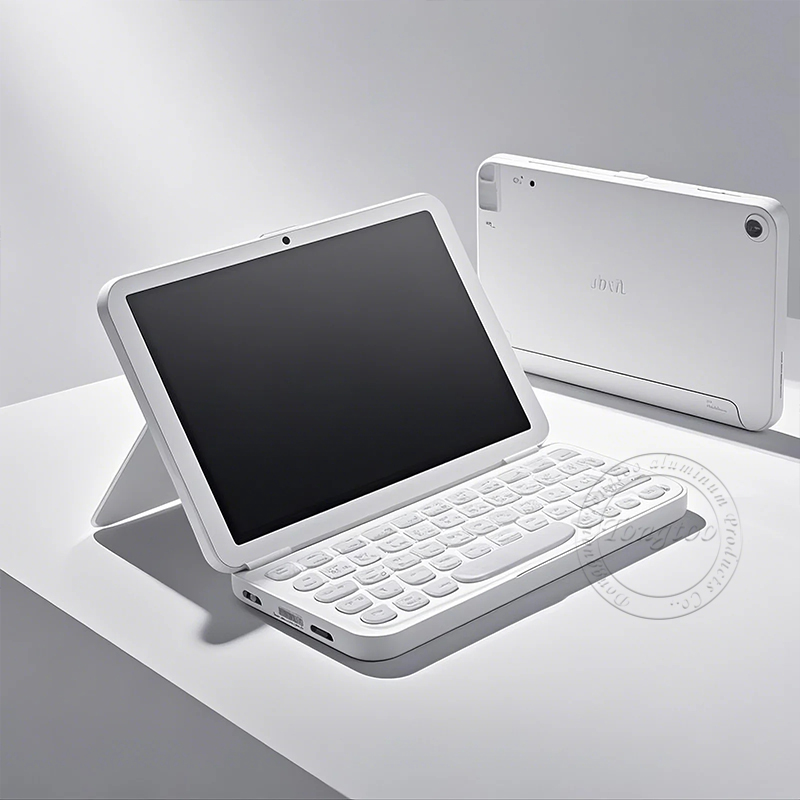
Aluminum Alloy Enhances Durability and Design in Learning Machine Housing
As the demand for durable, lightweight, and visually appealing educational devices increases, aluminum alloy is becoming a preferred material for learning machine housing. Known for its excellent mechanical properties and sleek aesthetic, aluminum alloy offers a compelling solution for manufacturers aiming to improve both functionality and user experience in smart educational tools.
-
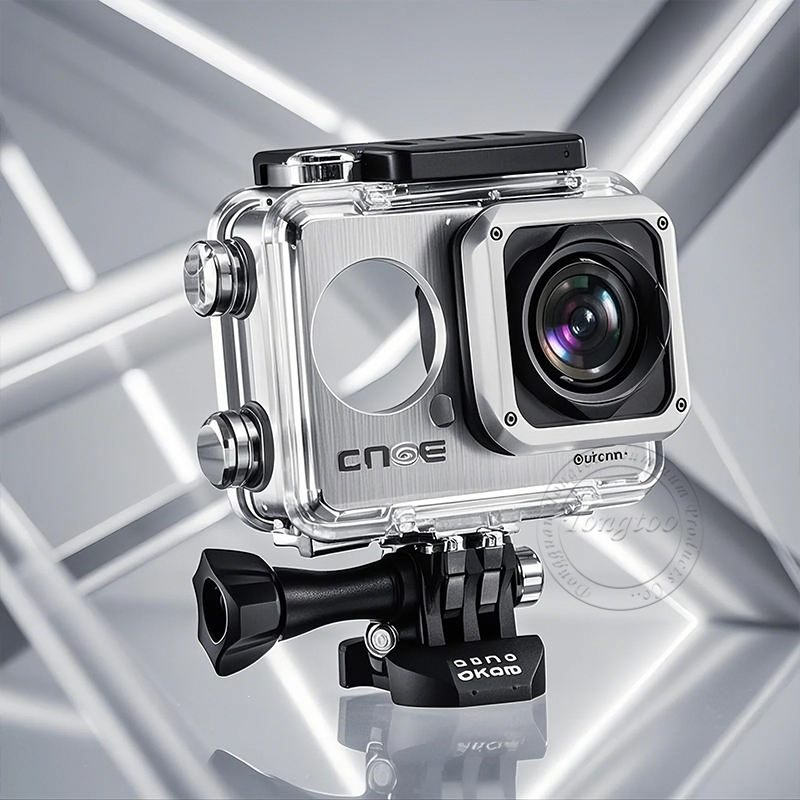
Aluminum Alloy Enhances Durability and Design in Sports Camera Housings
In the fast-evolving world of sports and action photography, the demand for rugged, lightweight, and aesthetically pleasing camera housings is higher than ever. Aluminum alloy has quickly become the material of choice for many leading manufacturers of sports cameras, thanks to its exceptional combination of strength, portability, and corrosion resistance.
-
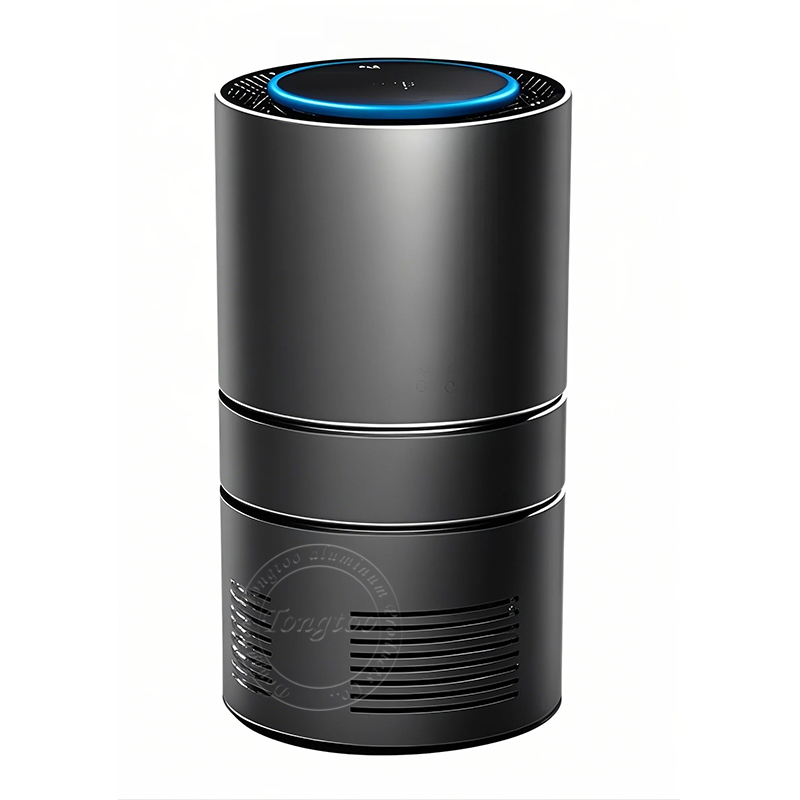
Aluminum Alloy Gains Ground in the Home Appliance Industry
In recent years, aluminum alloy has emerged as a key material driving innovation and sustainability in the home appliance sector. Known for its excellent strength-to-weight ratio, corrosion resistance, and aesthetic appeal, aluminum alloy is now widely used in the production of refrigerators, washing machines, air conditioners, microwave ovens, and more.
-
Aluminum Alloy: A Versatile Material Transforming Multiple Industries
Aluminum alloy has become one of the most widely used materials across a variety of industries due to its exceptional properties—lightweight, corrosion-resistant, thermally conductive, and highly recyclable. From consumer to electronics, aluminum alloy plays a pivotal role in driving innovation, improving efficiency, and enabling sustainable development.
-
TongToo Aluminum Products: A Trusted Supplier of High-Quality Aluminum Alloy Products
As global demand for lightweight, durable, and corrosion-resistant materials grows, TongToo Aluminum Products has emerged as a reliable and innovative aluminum alloy products supplier. With a strong commitment to quality, precision engineering, and customer satisfaction, the company has established itself as a leading name in the aluminum industry.
-
Exploring the Diverse Types of Aluminum Alloy and Their Industrial Applications
Aluminum alloys are indispensable in modern manufacturing, offering a wide range of properties that suit various industrial needs. These alloys are broadly categorized into two types: wrought aluminum alloys and cast aluminum alloys. Each type has multiple series and grades, tailored for specific mechanical requirements and processing methods.
-
Aluminum Alloy Gains Momentum Across Industries for Its Strength and Sustainability
Aluminum alloy is emerging as a key material in modern industrial applications due to its exceptional combination of lightweight, strength, corrosion resistance, and recyclability. As industries move toward more sustainable and efficient solutions, the demand for aluminum alloy products is growing rapidly in sectors such as automotive,construction, and consumer electronics.
-
Aluminum Alloy in 3C Electronics: Powering Innovation and Premium Design
In the fast-evolving world of 3C electronics—computers, communications, and consumer electronics—aluminum alloy has become a cornerstone material, driving both performance and aesthetics. Known for its lightweight, durability, and superior heat dissipation, aluminum alloy is widely used in a range of high-end electronic devices. Key applications include Anodized Aluminum Products Aluminum Alloy TV Frames, Precision Machined Aluminum Alloy Display Brackets, High-Strength Protective Aluminum Alloy Display Frames, and Aluminum Alloy Set-Top Box Shells.
-
Expanding Role of Aluminum Alloy in the Automotive Industry: Key Components Leading the Transformation
As the automotive industry shifts toward lighter, more energy-efficient, and sustainable vehicles, aluminum alloy has emerged as a crucial material driving innovation. Its excellent strength-to-weight ratio, corrosion resistance, and recyclability make it ideal for a wide range of automotive components. Among the most impactful applications are the Automobile Aluminum Alloy Battery Tray, Interior Panel, Pedal, and Drive Shaft.
-
Application of Aluminum Alloy: A Key Material Powering Modern Industry
Aluminum alloy has become one of the most versatile and widely used materials across various industries, thanks to its exceptional properties such as lightweight, strength, corrosion resistance, and recyclability. From automotive to electronics and consumer goods, the application of aluminum alloy is reshaping modern manufacturing and design.
-
Application of Aluminum Alloy in Electric Toothbrushes: Merging Durability with Design
As consumers demand smarter, sleeker, and more durable personal care products, aluminum alloy is emerging as a preferred material in the design and manufacturing of electric toothbrushes. Its application is revolutionizing both the functional performance and aesthetic appeal of these everyday devices.
-
Application of Home Appliances Aluminum Products: Enhancing Efficiency and Modern Design
In today’s home appliance industry, aluminum has become an indispensable material, transforming the way products are designed, manufactured, and used. The application of aluminum products in home appliances is rapidly expanding due to their lightweight nature, high thermal conductivity, corrosion resistance, and sleek modern appearance.
-
What Products Are Made from Aluminum? Exploring the Everyday Applications of a Versatile Metal
Aluminum has become one of the most widely used metals across the globe, thanks to its lightweight, corrosion resistance, and excellent thermal and electrical conductivity. From household items to industrial machinery, aluminum is everywhere. But what products are actually made from aluminum? The answer spans a wide range of industries—automotive, construction, electronics, and consumer goods.
-
TongToo Emerges as a Leading Aluminum Profile Manufacturer in Global Markets
As the global demand for lightweight, durable, and sustainable building materials rises, aluminum profiles have become essential across industries such as construction, transportation, electronics, and renewable energy. Among the rising stars in this field is TongToo, a reputable aluminum profile manufacturer known for its high-quality products, advanced production capabilities, and customer-oriented service.
-
The Growing Role of Aluminum Alloy Medical Equipment Parts in Modern Healthcare
In the evolving landscape of medical technology, the demand for lightweight, durable, and corrosion-resistant materials has never been greater. Among the most widely adopted materials in recent years is aluminum alloy, which is now playing a crucial role in the design and manufacturing of medical equipment parts. From diagnostic tools to surgical instruments and mobility devices, aluminum alloy medical equipment parts are helping transform healthcare with improved functionality, safety, and efficiency.
-
Key Considerations in CNC Precision Parts Processing: Ensuring Accuracy and Efficiency
As global industries continue to evolve toward automation and high-precision manufacturing, CNC precision parts processing has become a cornerstone of modern production. From aerospace to automotive, medical devices to electronics, CNC machining enables manufacturers to produce complex components with extreme accuracy and consistency.
-
Exploring the Expanding Applications of Aluminum Alloy Products in Modern Industries
In recent years, aluminum alloy has become a critical material across a wide range of industries due to its excellent combination of strength, lightweight properties, corrosion resistance, and aesthetic flexibility. From electric vehicles to consumer electronics and urban infrastructure, the demand for aluminum alloy products continues to surge. Among the most notable innovations are the Automobile Aluminum Alloy Battery Tray, Aluminum Alloy Floor Lamp Pole, and Aluminum Alloy Hair Straightener Plate—each representing a unique use case that showcases the versatility of this advanced material.
-
How To Reshape The Reliability Of Medical Devices With Aluminum Alloy Technology
This is the core battlefield for iterative upgrades of products such as aluminum alloy medical device boxes, aluminum alloy medical smart medicine cabinets, and medical trolley accessories.
-
Aluminum Profile CNC Machining Customization: The Core Solution For High-Precision Manufacturing
In modern manufacturing, aluminum profile CNC machining has become the core technology for the production of precision parts. This technology occupies an important position in the fields of automobiles, 3C electronics, etc.
-
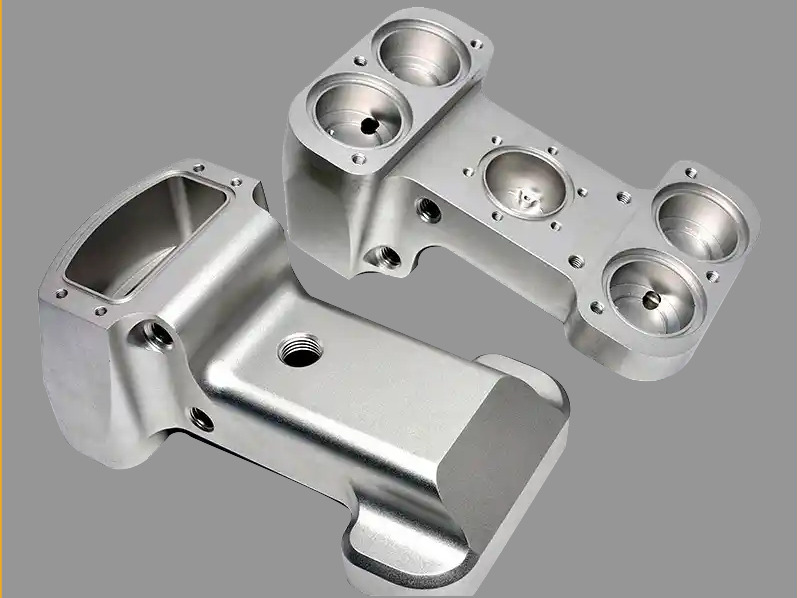
Aluminum Machining Cutting Depth: How To Correctly Choose Aluminum Machining Tools
Aluminum machining cutting depth refers to the depth of cutting of aluminum materials during a cutting process. According to the characteristics of various aluminum alloy materials and different processes and processing contents, the respective cutting depths are different.
-
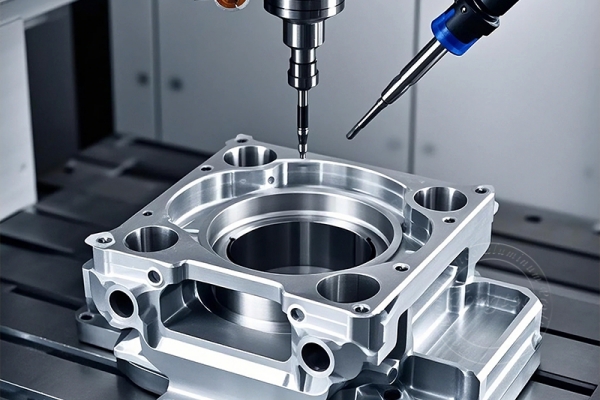
CNC Machining: Opening A New Era Of Precision Manufacturing
CNC machining achieves high-precision cutting, engraving and molding of various materials through computer digital control. Whether it is complex geometric shapes or strict dimensional tolerance requirements, CNC machining can easily cope with it.
-
A Batch Of High-Quality Products That Embody The Team's Hard Work Have Been Shipped Successfully!
From the first step of mold manufacturing, we have devoted full attention. Each mold has been carefully carved to strive for accuracy and lay a solid foundation for product molding. In the CNC precision processing link, advanced equipment and superb technology are combined to strictly control every detail and not miss the slightest error.
-
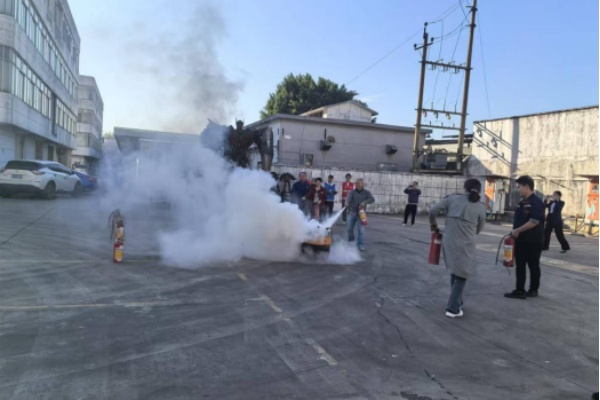
Fire Drills Build A Strong Defense Line, And Safety Awareness Is Deeply Rooted In The Hearts Of The People
In order to enhance the fire safety awareness and emergency response capabilities of all employees, on October 25, 2024, the company organized a comprehensive fire drill, in which all employees participated, and the CNC precision machining workshop also responded positively.
-
In-Depth Discussion, Jointly Drawing The Company's Development Blueprint
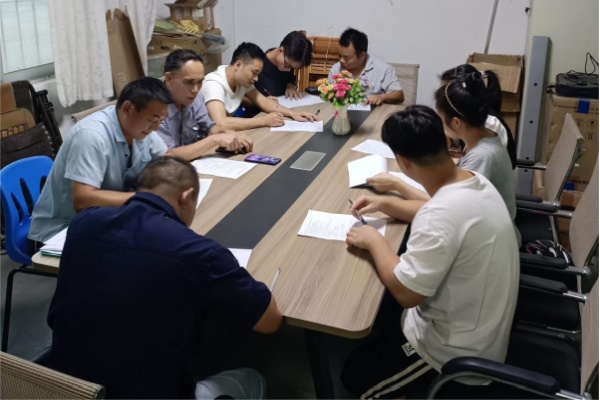
On January 12, 2025, the company held a crucial technical seminar to gather wisdom and promote high-quality business development. The backbones and technical elites of various departments of the company gathered together to conduct in-depth exchanges on core businesses such as CNC precision machining, mold design, injection molds, and surface treatment.
-
Dongguan Tongtoo Aluminum Products Co., Ltd. Puts New Equipment Into Production, Leading A New Journey Of Development
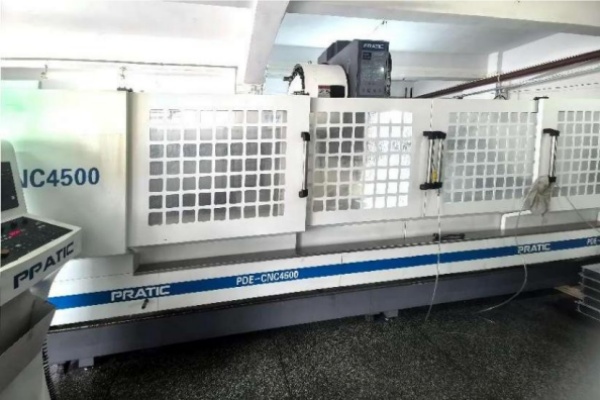
Recently, Dongguan Tengtu Aluminum Products Co., Ltd. has ushered in a new opportunity for development. The company has added a Prady 4500CNC machining center and two Jugao TC1365 high-speed drilling and tapping machining centers. After completing the trial run, they were officially put into production. This milestone event has injected new vitality into the company's development.
-
How Much Precision Can Five-Axis CNC Machining Achieve
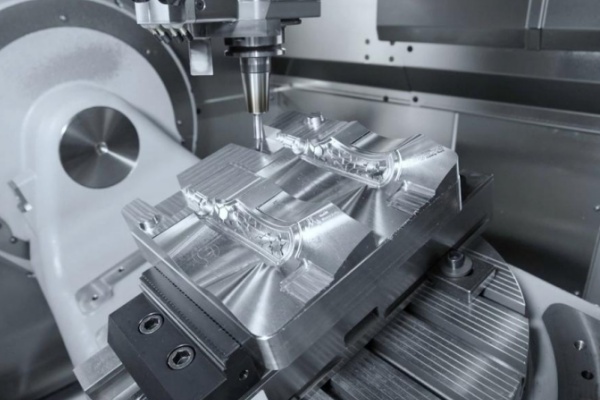
The machining precision of five-axis linkage machine tools can reach 0.002 mm, and this precision standard is of great significance in the field of precision manufacturing.


